 Inside Asian Packaging
How Asian Packaging Industries Manufactures High-Quality Corrugated Boxes
In today's competitive manufacturing environment, packaging is much more than just a box. It protects products, supports efficient logistics,…
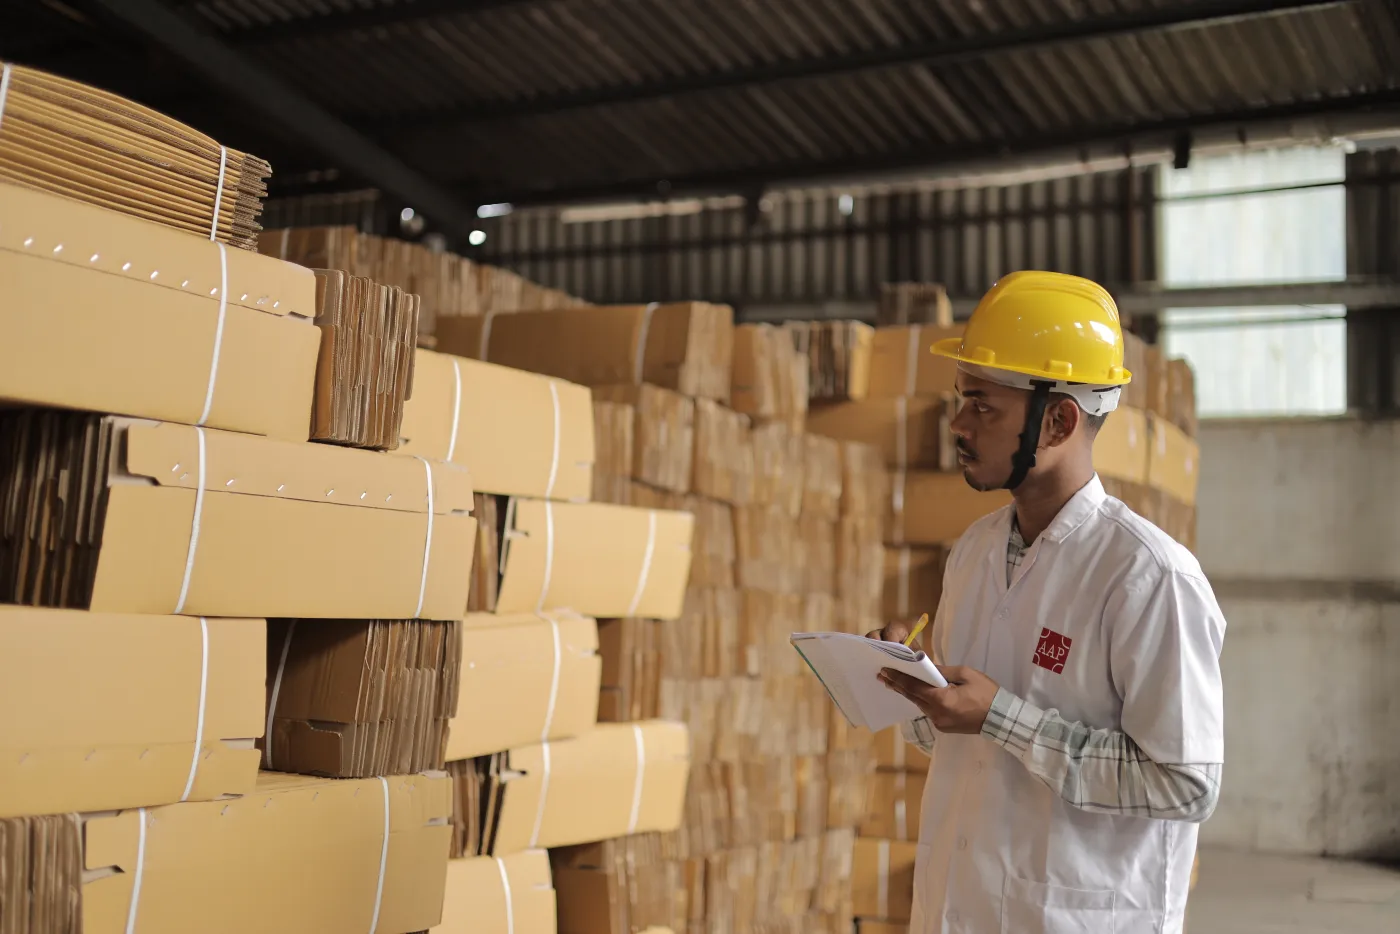
A corrugated box may look simple from the outside, but its ability to protect products depends on precise engineering and rigorous quality control. Even small variations in paper quality, moisture content, adhesive bonding, or board strength can affect packaging performance during transportation and storage.
At Asian Packaging Industries, we believe quality cannot be inspected only after production—it must be built into every stage of manufacturing. That is why we operate a fully equipped in-house quality testing laboratory, where every batch of raw materials and finished packaging undergoes comprehensive testing before reaching our customers.
This commitment to quality helps businesses reduce product damage, improve logistics efficiency, lower packaging costs, and maintain customer confidence.
Packaging failures can be expensive.
A weak corrugated box can lead to:
These problems often cost far more than the packaging itself.
Quality testing ensures that every corrugated box performs exactly as intended throughout the supply chain.
At Asian Packaging Industries, quality is not limited to the final inspection.
It begins with:
This systematic approach ensures consistency from the first box to the last.
Our in-house laboratory is designed to evaluate every critical property of corrugated packaging.
We test:
Every test helps us verify that the packaging meets customer specifications and industry standards.
The GSM Test measures the weight of paper per square meter.
Why it matters:
Customers receive packaging manufactured with the correct paper grade every time.
The Burst Factor Test measures the paper’s resistance to rupture under pressure.
Benefits:
High BF paper provides greater durability during handling and shipping.
The Bursting Strength Test evaluates the overall strength of the corrugated board.
This test helps ensure:
One of the most important tests for corrugated packaging.
ECT measures how much vertical load a corrugated board can withstand before collapsing.
Benefits include:
High ECT values result in better stacking strength.
The BCT measures how much weight a completed corrugated box can safely support.
This is especially important for:
Proper compression strength reduces carton collapse and product damage.
The Cobb Test measures the water absorption characteristics of paper.
Why it matters:
This is particularly important for humid climates and sea shipments.
Paper naturally absorbs moisture from the environment.
Excess moisture can reduce packaging strength.
Our Moisture Content Test helps ensure:
The strength of the bond between liners and fluting is critical.
The Pin Adhesion Test evaluates:
Strong bonding improves the structural performance of corrugated boards.
Every corrugated box is checked for:
Accurate dimensions ensure efficient packing and reliable product protection.
For printed packaging, we verify:
This helps customers maintain a professional brand image.
Having our own laboratory allows us to detect and correct issues before products leave the factory.
This provides several advantages.
Every batch is manufactured to the same high standards.
Any variation can be identified immediately, reducing production errors.
Customers receive stronger, more reliable packaging.
Proper testing minimizes carton collapse and transportation damage.
Reliable packaging results in fewer complaints and returns.
Our testing laboratory supports packaging for many industries.
Ensures cartons withstand high-volume distribution.
Maintains dimensional accuracy and reliable protection.
Verifies heavy-duty packaging performance.
Ensures safe transportation for delicate equipment.
Tests packaging durability for demanding logistics conditions.
Confirms moisture resistance and stacking performance for international shipping.
Quality is monitored throughout manufacturing.
Every paper reel is checked before production.
Machine settings are continuously monitored during manufacturing.
Samples are tested throughout production.
Every batch undergoes final quality verification before dispatch.
This multi-stage inspection process ensures consistent performance.
Businesses partnering with Asian Packaging Industries experience:
✔ Lower product damage
✔ Better warehouse stacking
✔ Reduced transportation losses
✔ Improved customer satisfaction
✔ Consistent packaging quality
✔ Better brand reputation
✔ Fewer product returns
✔ Long-term cost savings
Reliable packaging contributes directly to business success.
Our laboratory also supports:
Testing is not only about maintaining quality—it also helps us develop better packaging solutions for the future.
Our commitment to quality extends beyond manufacturing.
Our strengths include:
Every packaging solution is tested to ensure it meets our quality standards before reaching our customers.
Our quality engineers recommend:
✔ Never select packaging based only on price.
✔ Verify packaging specifications through laboratory testing.
✔ Perform compression testing for stacked products.
✔ Consider moisture conditions when designing export packaging.
✔ Review packaging performance regularly.
✔ Partner with manufacturers that have dedicated quality laboratories.
Quality testing prevents problems before they reach your customers.
Quality testing ensures that corrugated boxes have the required strength, durability, moisture resistance, and dimensional accuracy to protect products throughout transportation and storage.
We perform GSM, Burst Factor (BF), Bursting Strength, Edge Crush Test (ECT), Box Compression Test (BCT), Cobb Test, Moisture Content Test, Pin Adhesion Test, Dimensional Inspection, and Print Quality Inspection.
In-house testing allows faster quality verification, early problem detection, consistent production quality, reduced packaging failures, and improved customer satisfaction.
The BCT measures how much weight a completed box can safely withstand, ensuring reliable stacking during warehousing and transportation.
Yes. Proper testing ensures packaging is correctly engineered—not under-designed or over-specified—helping businesses reduce product damage, optimize material usage, and lower overall packaging costs.
Quality testing is one of the most critical factors in manufacturing reliable corrugated packaging. From raw material inspection to final product verification, every test performed in our in-house laboratory helps ensure that each corrugated box delivers consistent strength, durability, and performance. This systematic approach minimizes packaging failures, protects products throughout the supply chain, and provides customers with confidence in every shipment.
At Asian Packaging Industries, our investment in advanced testing equipment, experienced quality professionals, and continuous process improvement reflects our commitment to excellence. By combining comprehensive laboratory testing with modern manufacturing technology and customized packaging engineering, we deliver packaging solutions that protect products, reduce costs, and support the long-term success of our customers.
Need this specified for your own product?
Inside Asian PackagingIn today's competitive manufacturing environment, packaging is much more than just a box. It protects products, supports efficient logistics,…
6 min read Inside Asian Packaging
Every successful business has a story. Some are built on technology, while others are built on vision, hard work, and trust. At Asian Packaging…
6 min read Inside Asian Packaging
Behind every high-quality corrugated box is a world-class manufacturing facility. Modern packaging requires far more than paper and machines—it…
6 min read